Home / Our plant
Precision is programmed, not inspected.
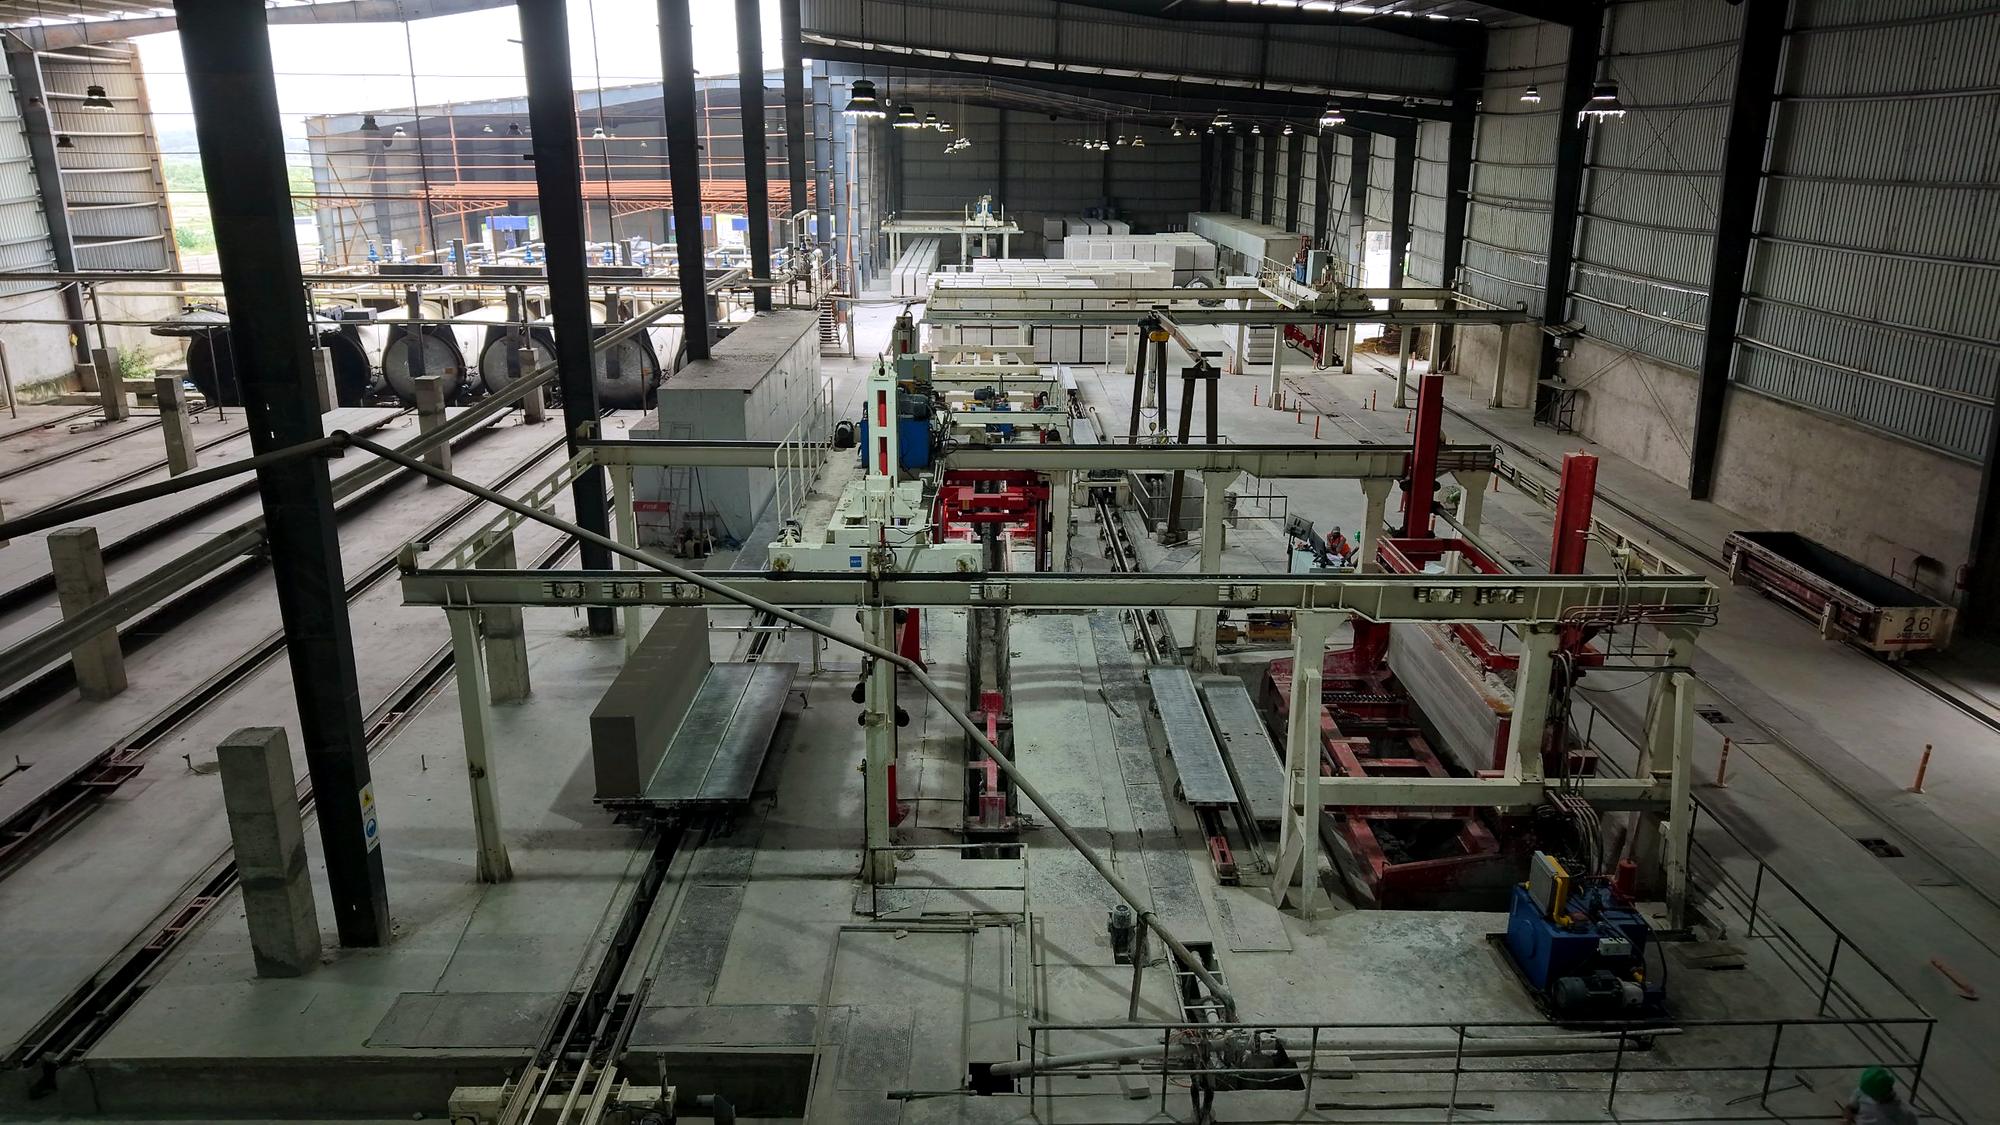
The AAC industry struggles with inconsistency, operator dependency and short-term decisions. Brickcem was set up in 2024 to remove them — with a fully automatic plant at Salod, near Kapadvanj in Kheda district, built to run reliably for decades.
The line, station by station
Raw material → mixing → casting → precision cutting → steam curing and autoclaving. The same programme runs for the first block of the day and the last.
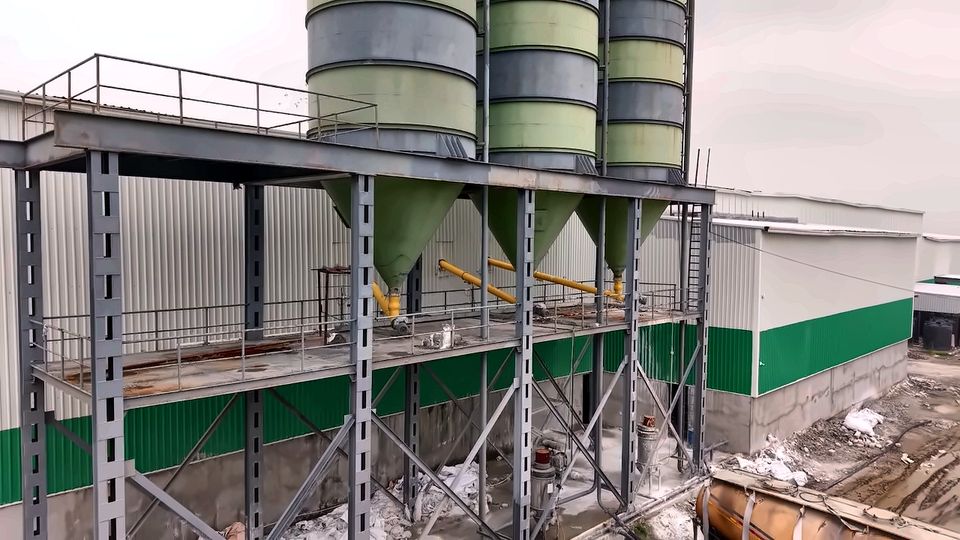 Raw materialBulk handling instead of manual feeding. Fly ash and sand are stored apart and discharged in measured ratios, which is what keeps density and strength repeatable.
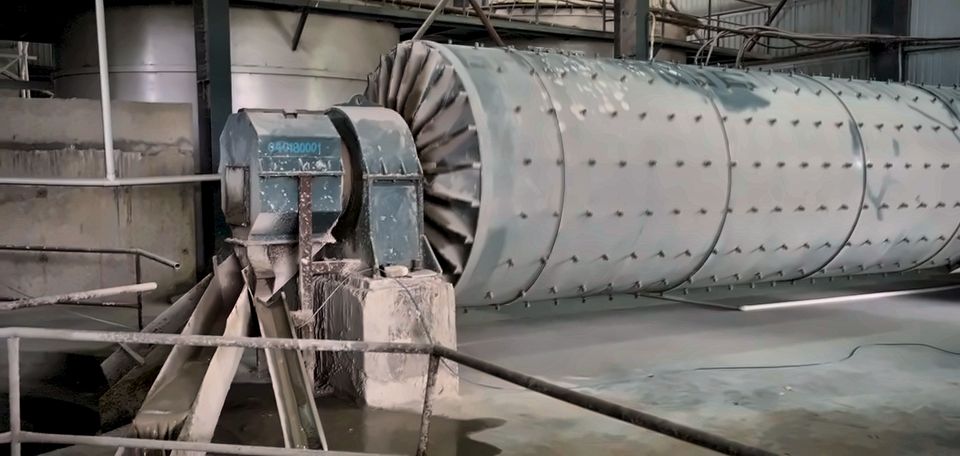 MixingKEDA dosing and mixing: lime, cement, gypsum, water and a trace of aluminium powder, to a fixed recipe.
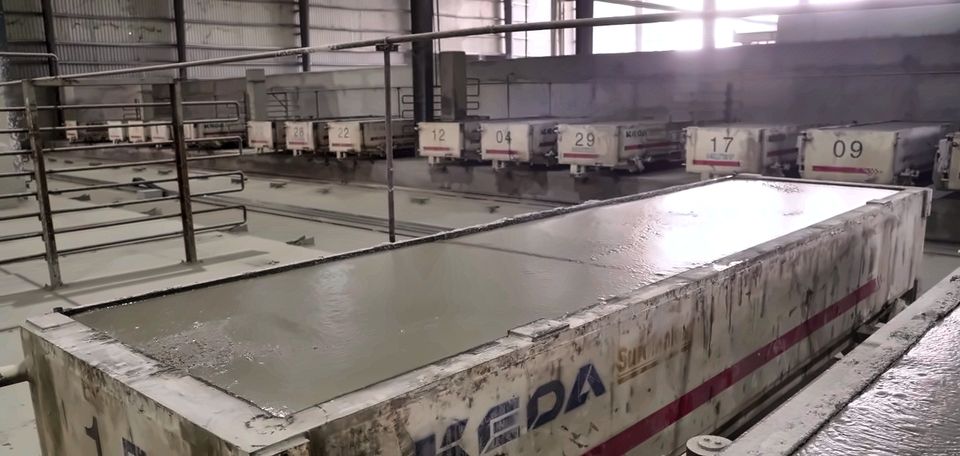 CastingThe slurry is cast into moulds, where it rises and sets into a firm green cake.
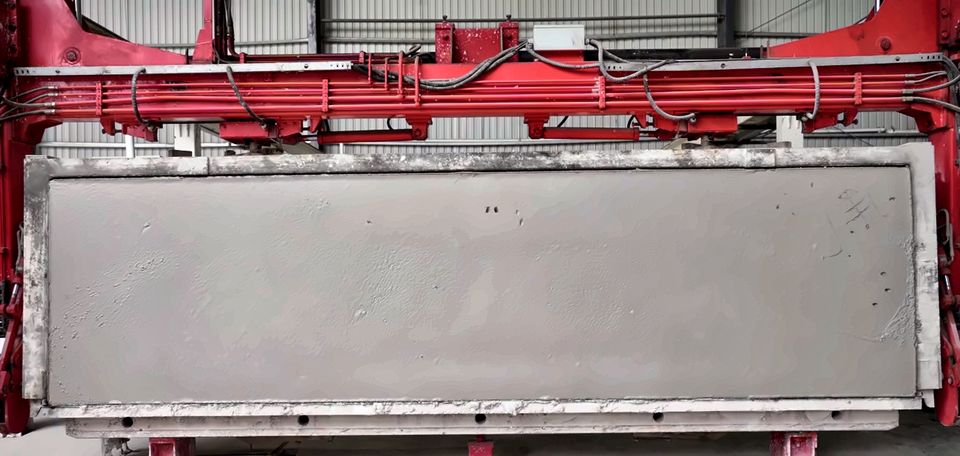
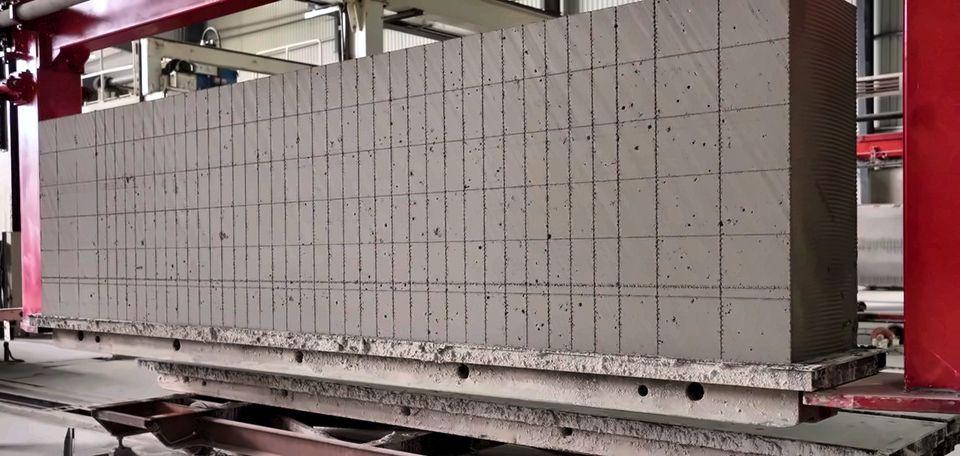
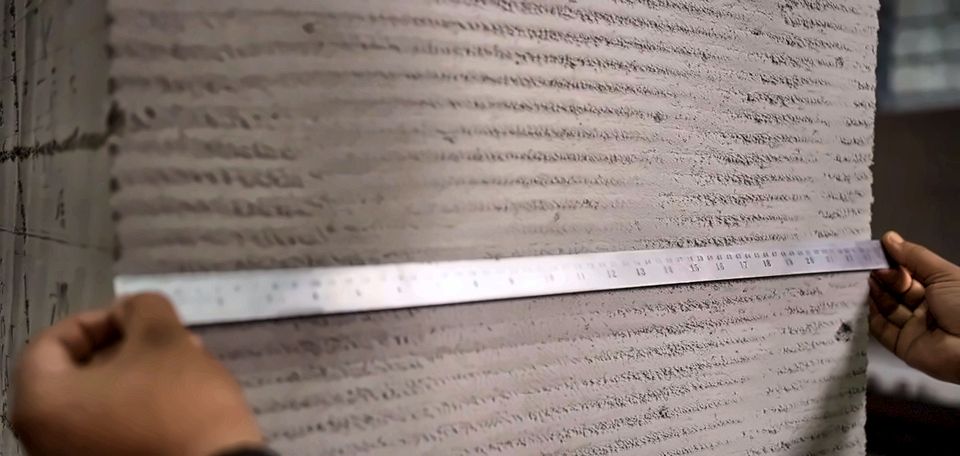
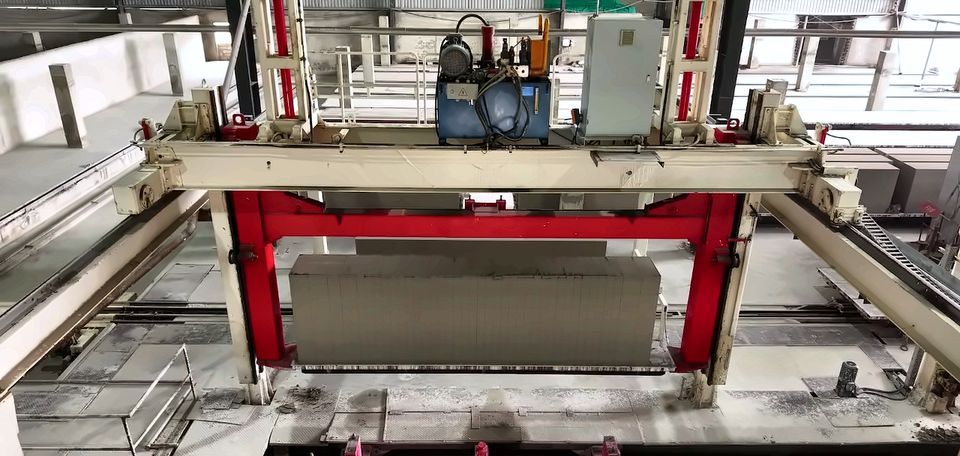
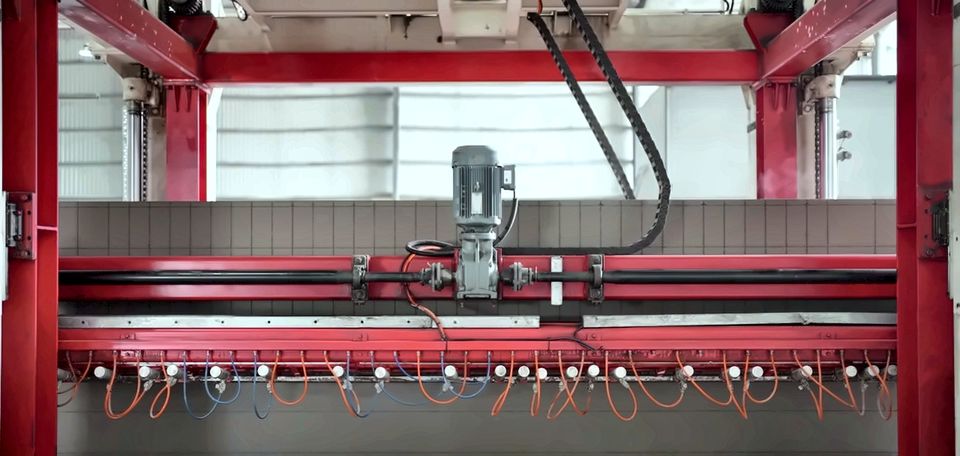 Precision cuttingAn automatic gantry cuts the cake with wires to a tolerance of ±2 mm.
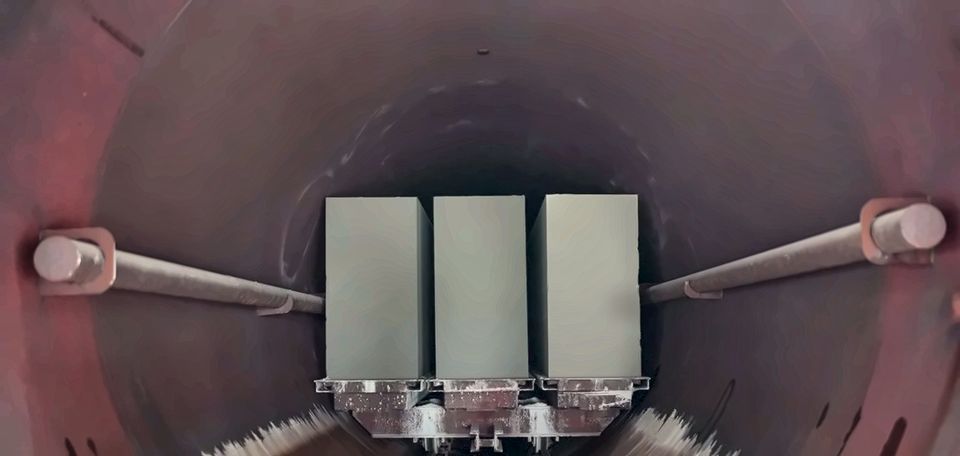
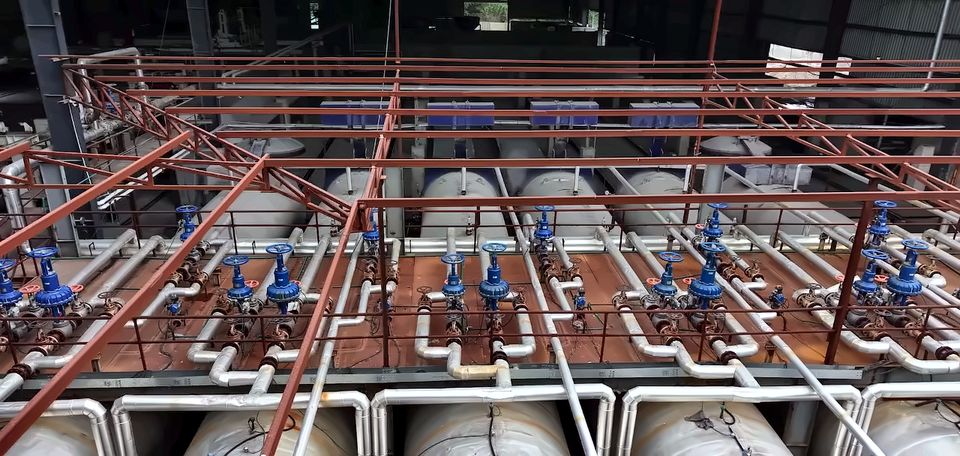
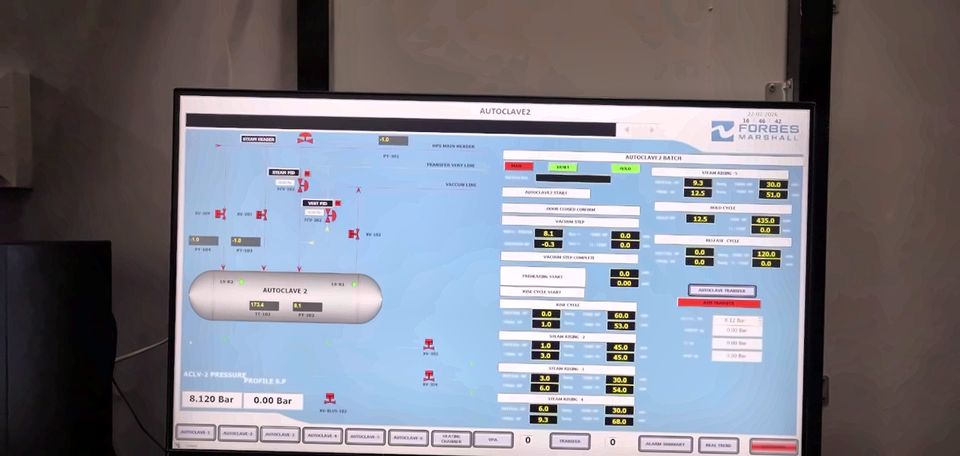
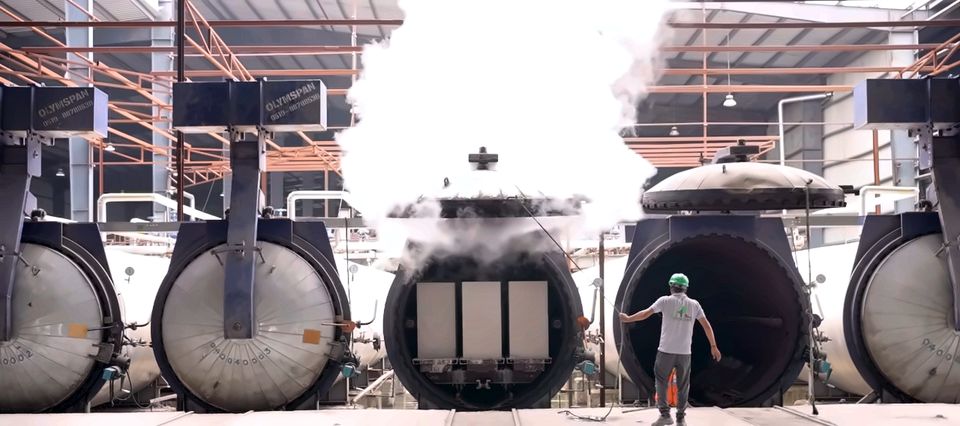 AutoclavingHigh-pressure steam curing with Forbes Marshall and Olymspan systems, the same cycle every time.
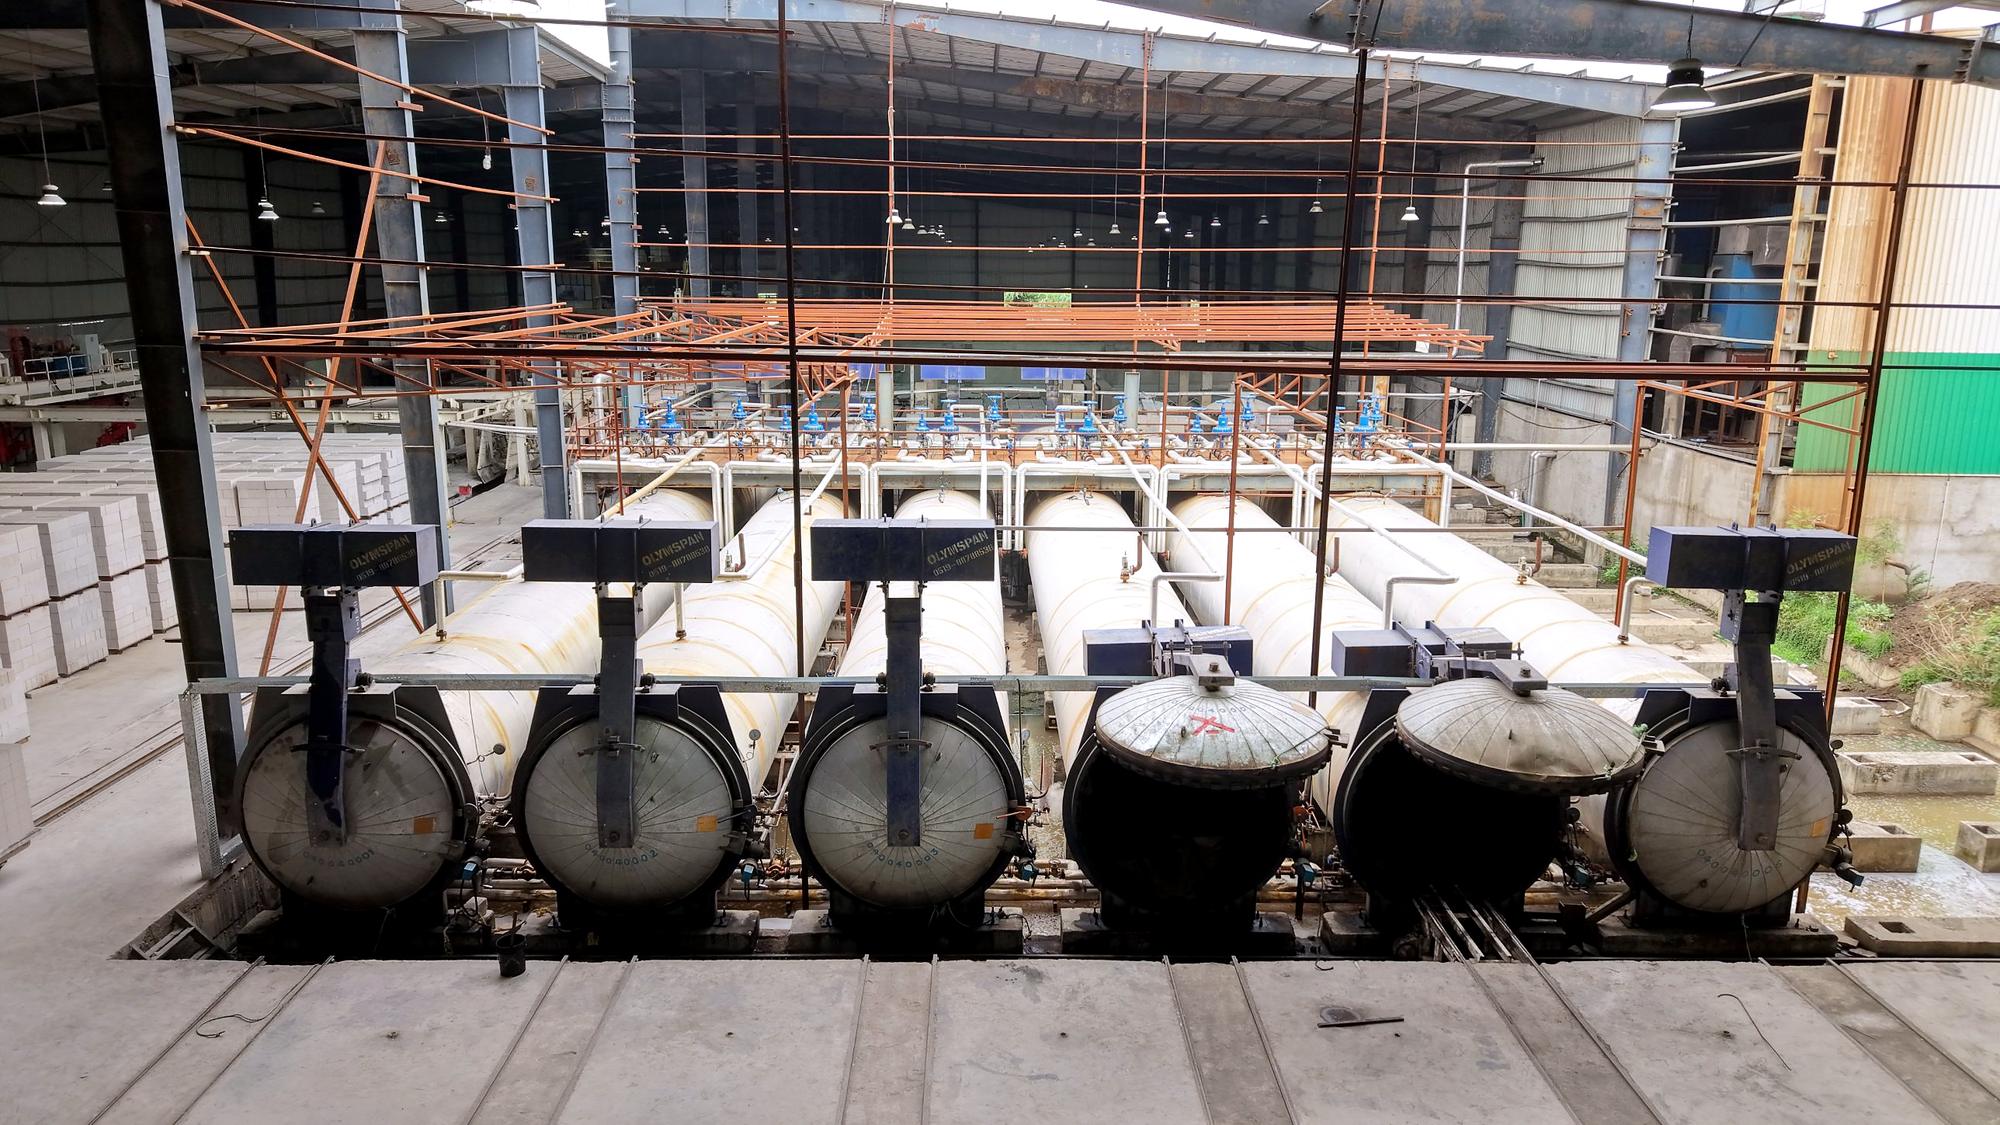
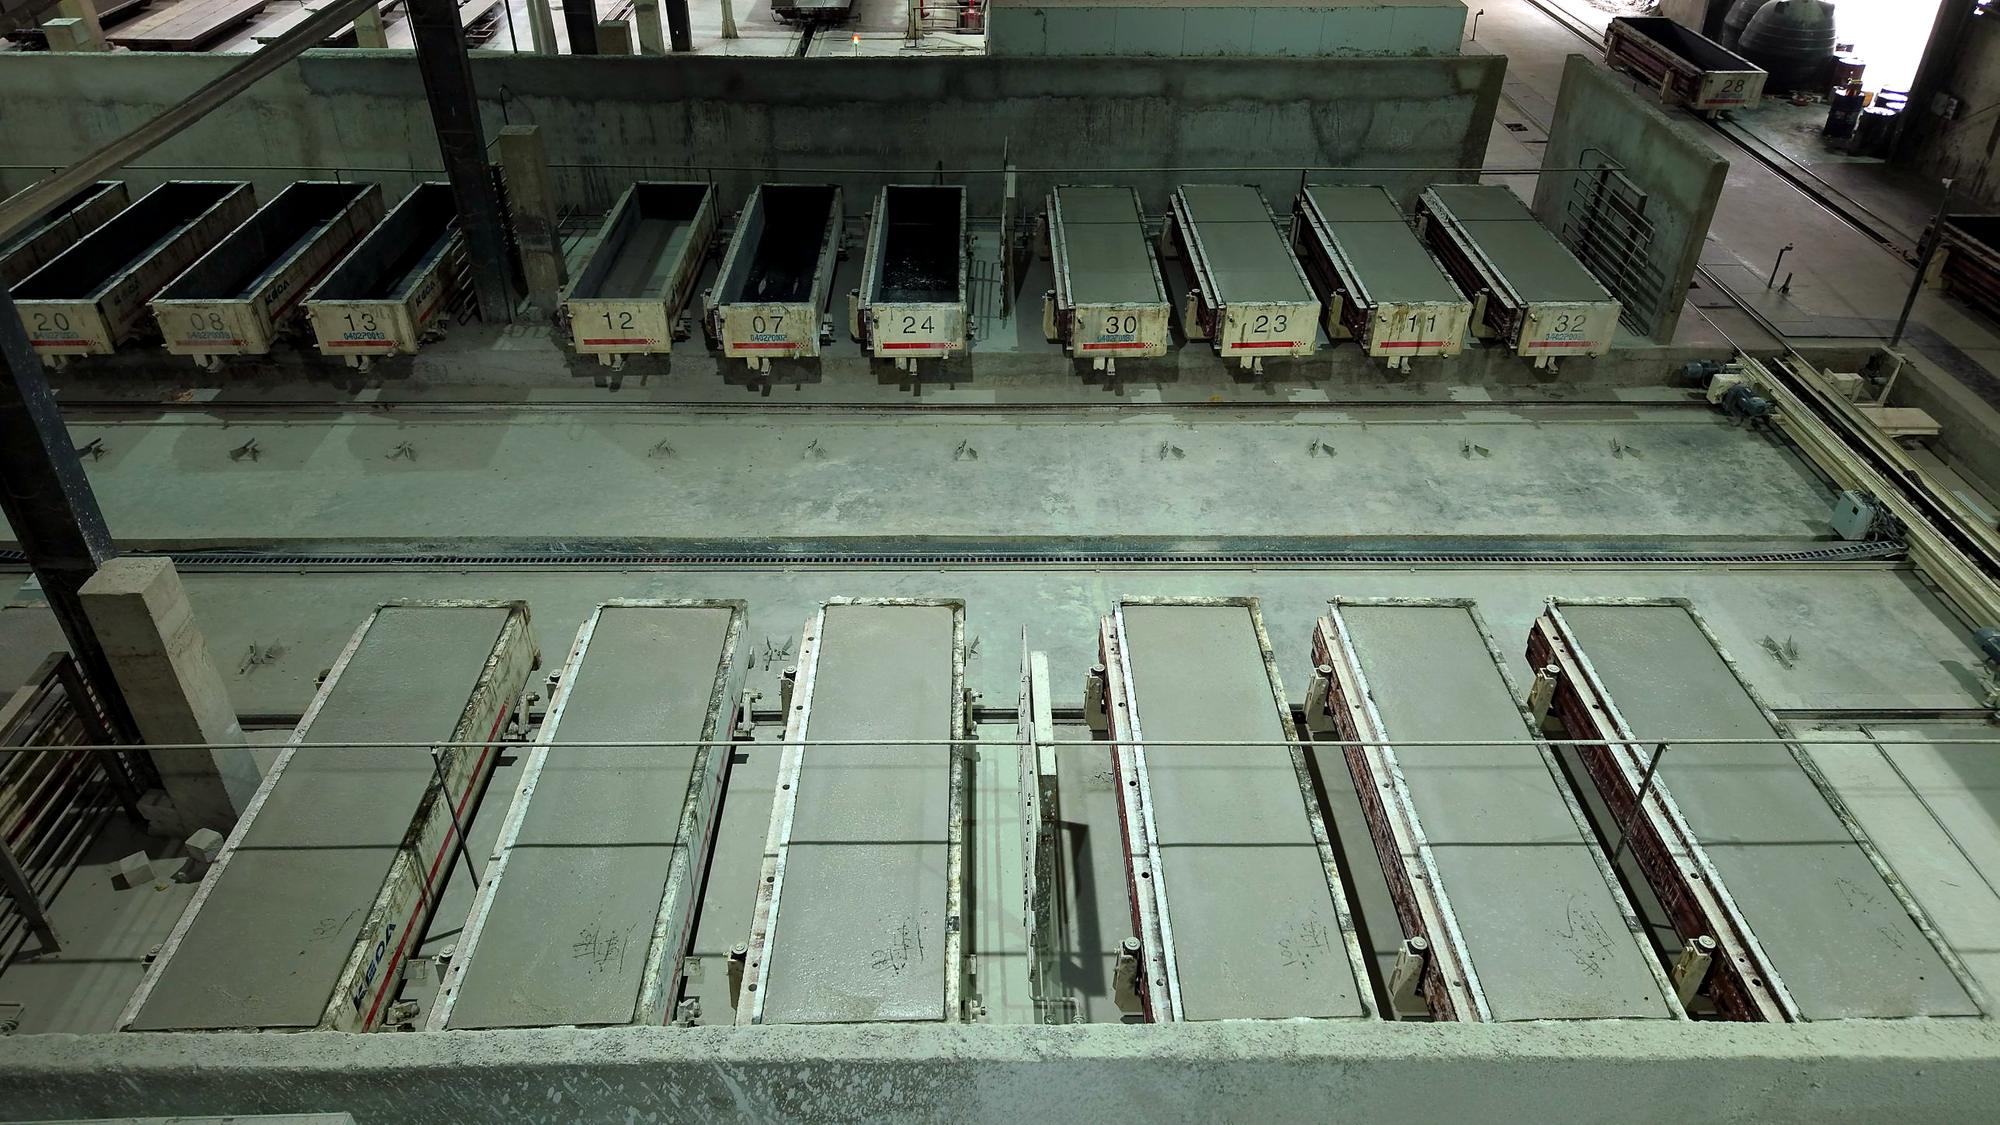
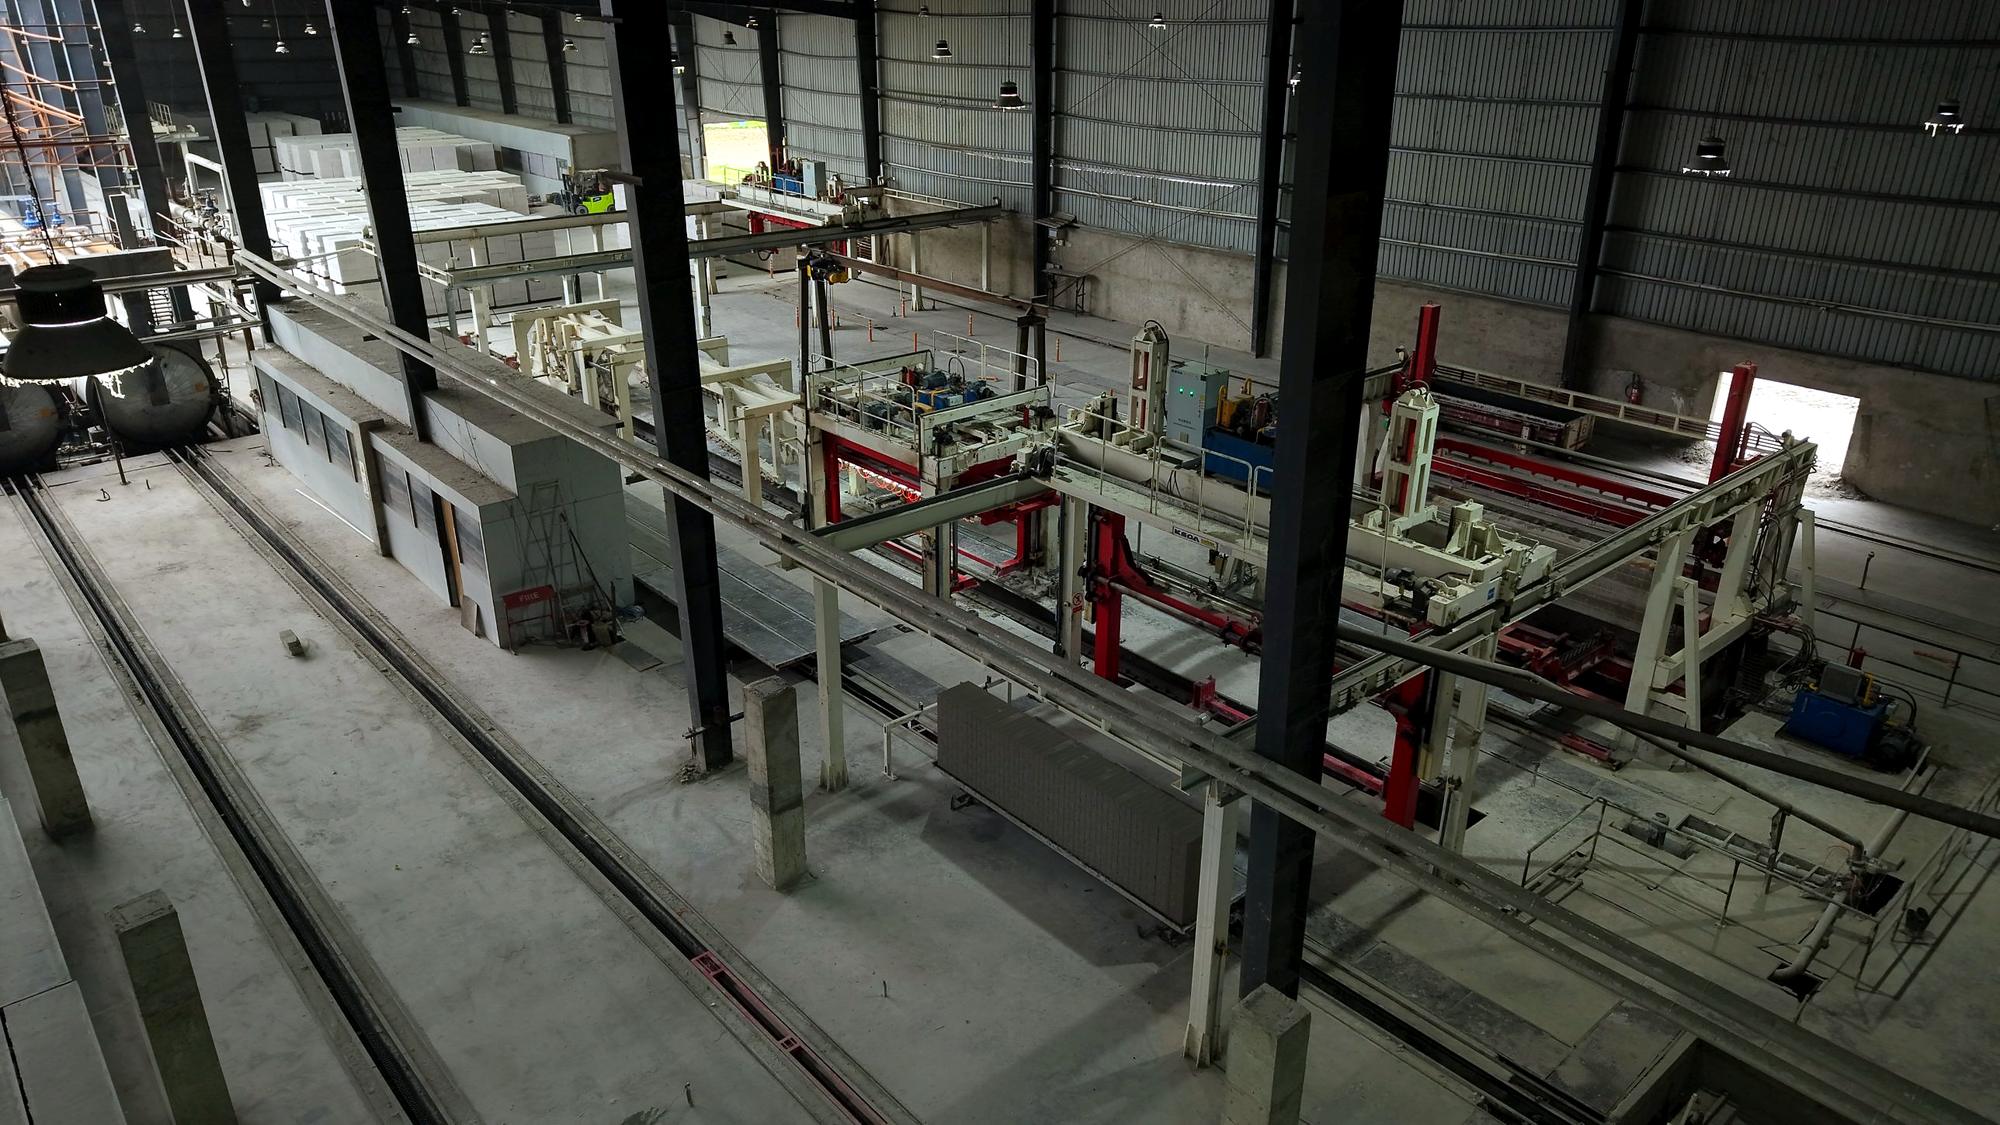
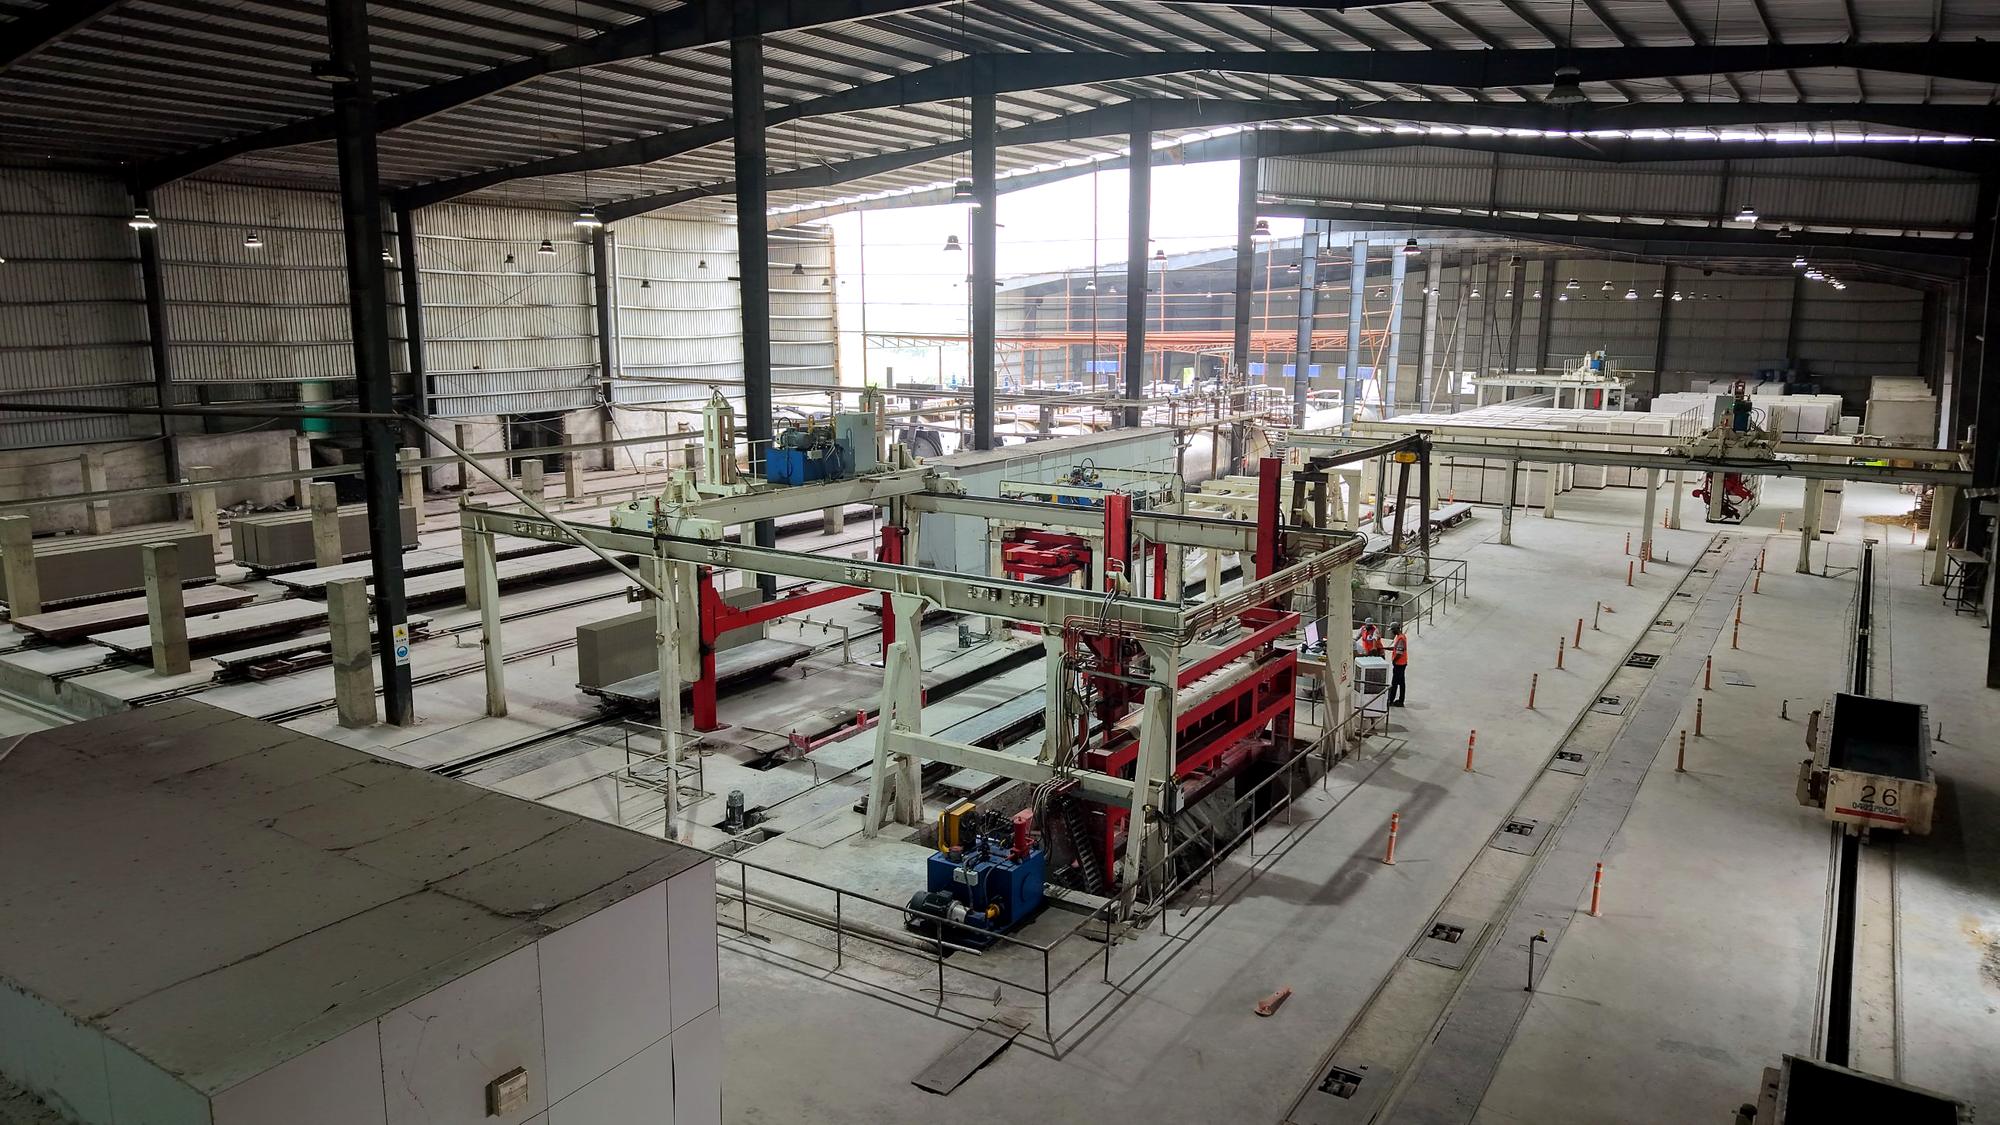
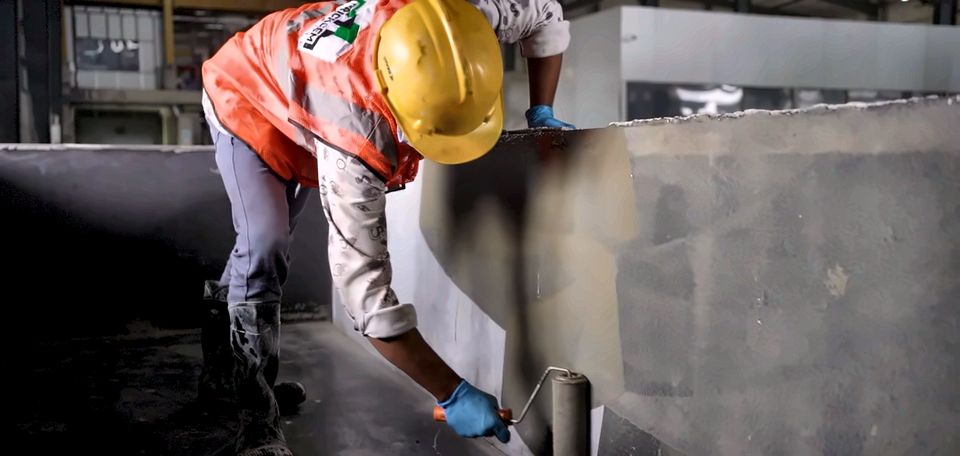
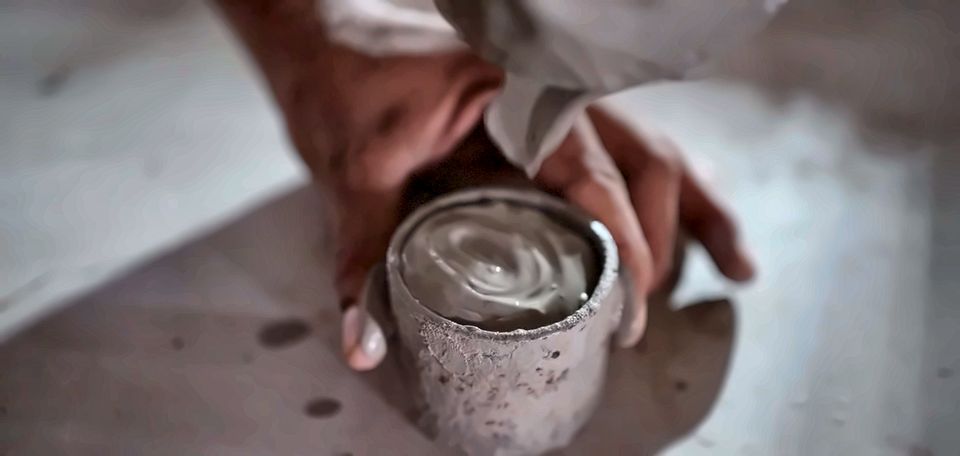
Eight moments from the line
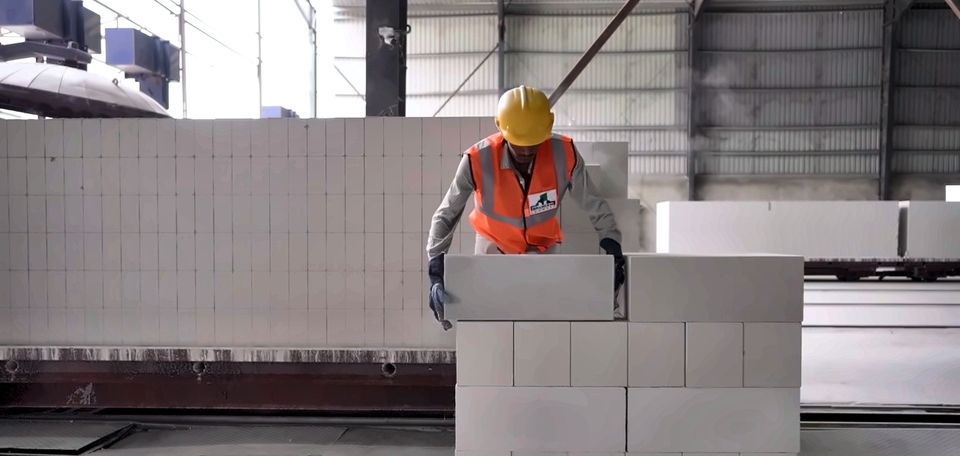
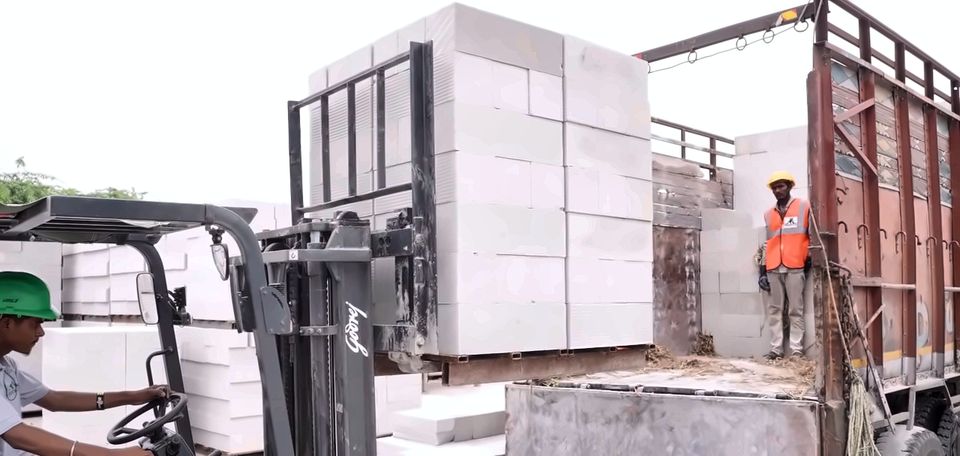
Stills from our factory film — the same process, every cake, every day.
Capital-intensive, on purpose
Machines chosen for control, not convenience.
The economics of precision
A block that is the right size saves money twice: once in the joint, once in the plaster.
Dimensional tolerance from the automatic gantry.
Up to this much less plaster and mortar, because thin-bed masonry works on true blocks.
Joints with AIWON Bond — the block and the mortar are designed together.
Block and bond engineered together, so walls go up faster with less waste.
Watch the factory film
Responsibility beyond the factory gate
We monitor the plant continuously and change the process when the data says so. We run it under ISO 9001 quality, ISO 14001 environmental and ISO 45001 health-and-safety management, and the blocks carry the GreenPro ecolabel.
Standards enforce discipline. We operate within them.
Visit the plant
Bring your engineer. See the line run, pull blocks from the stack, and take them to a lab of your choice.
Survey No. 316/1, 316/2, Kapadvanj – Ladvel Road, Salod, Ta. Kapadvanj, Dist. Kheda, Gujarat 387620